Brokensilenze in Heavy Industry: A Technical Guide to Valve Noise and Failure Diagnostics
April 17, 2026
Home+Brokensilenze in Heavy Industry: A Technical Guide to Valve Noise and Failure Diagnostics
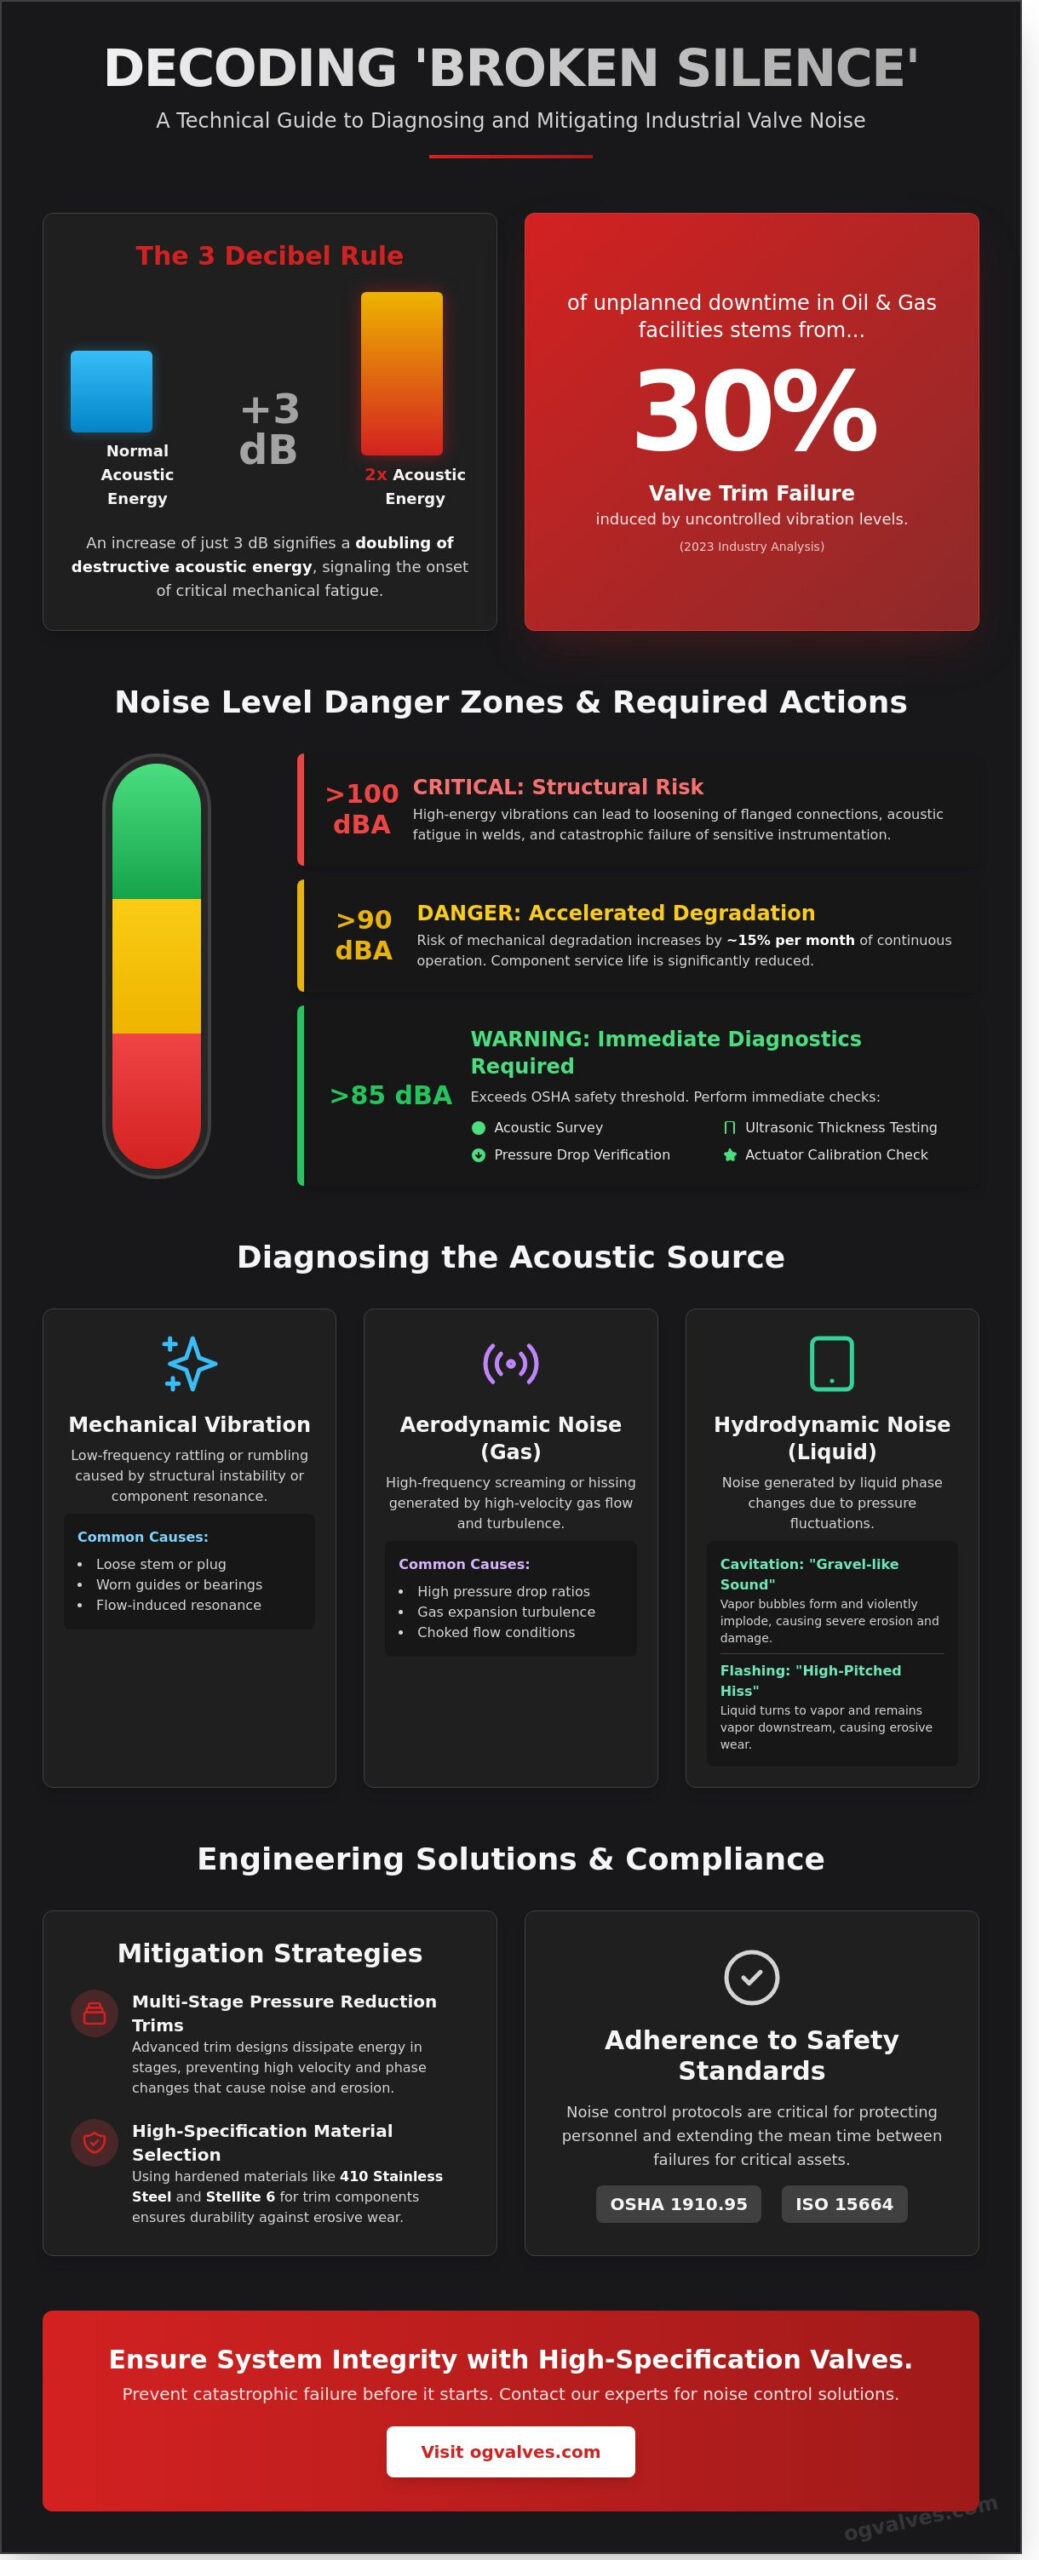
In high-pressure fluid systems, an increase of just 3 decibels signifies a doubling of acoustic energy, often marking the onset of critical mechanical fatigue. This transition from a steady-state operation to a state of brokensilenze indicates that internal components are already succumbing to destructive forces like cavitation or aerodynamic turbulence. Engineers recognize that excessive noise isn’t merely an environmental concern; it’s a clinical symptom of imminent hardware degradation. A 2023 industry analysis confirms that 30% of unplanned downtime in oil and gas facilities stems from valve trim failure induced by uncontrolled vibration levels.
You understand that maintaining system integrity requires more than just reactive maintenance. This technical guide provides the framework to accurately diagnose the root causes of valve noise and implement mitigation strategies that align with OSHA 1910.95 safety standards. You’ll learn to differentiate between cavitation and flashing while identifying the specific material grades and trim geometries required to prevent erosive wear. By following these diagnostic protocols, you’ll ensure your infrastructure maintains compliance with international noise regulations and achieves its projected service life without catastrophic failure.
Key Takeaways
Establish the technical baseline for acoustic integrity in high-pressure systems to recognize the immediate onset of mechanical distress.
Identify the mechanical vibrations and aerodynamic triggers that lead to a brokensilenze, allowing for rapid diagnostic intervention before catastrophic system failure.
Distinguish between the unique acoustic signatures of cavitation and flashing to prevent severe internal erosion and downstream piping damage.
Analyze engineering mitigation strategies, including the implementation of multi-stage pressure reduction trims, to counteract acoustic fatigue and ensure component durability.
Review the rigorous procurement and testing standards necessary for selecting high-specification valves that comply with international safety and performance benchmarks.
The Significance of ‘Broken Silence’ in Industrial Piping Systems
In high-pressure fluid transport, the baseline of acoustic integrity is defined by steady-state laminar or controlled turbulent flow. Engineers design these systems to operate within specific decibel ranges to ensure both mechanical longevity and operator safety. When a system exhibits brokensilenze, it signals a departure from designed operational parameters. This sudden transition from a controlled acoustic state to one of audible distress indicates that internal forces are no longer being managed by the valve’s trim or body geometry. High-stakes environments in the oil and gas sectors rely on these acoustic baselines to monitor the health of critical infrastructure without requiring immediate teardowns.
Noise levels are directly proportional to the internal state of valve components. A rise in decibels often correlates with increased fluid velocity or the onset of phase changes within the valve body. If a valve’s noise output exceeds the 85 dBA safety threshold, immediate diagnostic steps are required. These include:
Conducting a full acoustic survey using Class 1 sound level meters to map noise attenuation.
Performing ultrasonic thickness testing on downstream piping to check for erosion.
Verifying pressure drop ratios against the original valve specification sheets.
Inspecting the actuator calibration to ensure the plug is seated correctly.
When noise levels reach 90 dBA for an eight-hour time-weighted average, the risk of mechanical degradation increases by approximately 15% per month of continuous operation. Engineers shouldn’t ignore these signals, as they represent the physical manifestation of energy being dissipated through the valve structure rather than the process fluid.
Acoustic Signatures of Valve Distress
Differentiating between mechanical vibration and aerodynamic noise is vital for accurate failure diagnostics. Mechanical vibration usually stems from structural instability, such as a loose stem or worn guides, producing low-frequency rattling. Aerodynamic noise, conversely, is a high-frequency phenomenon occurring during gas expansion or high-velocity turbulence. In liquid services, understanding What is cavitation is essential for identifying the “gravel-like” sound that indicates vapor bubbles are imploding against the valve trim. The valve trim, often manufactured from hardened 410 stainless steel or Stellite 6, is responsible for maintaining silent operation. When the trim erodes, the resulting brokensilenze serves as a definitive early warning for seat leakage and compromised shut-off integrity.
Safety Standards for Industrial Noise Control
Compliance with OSHA 1910.95 and international standards like ISO 15664 is a prerequisite for legal and operational viability in heavy industry. Excessive noise isn’t just a workplace hazard; it’s a symptom of high-energy vibrations that threaten the structural integrity of forged steel components and welded joints. If a valve operates at 100 dBA or higher, the vibration can lead to the loosening of flanged connections and the failure of sensitive instrumentation. Acoustic fatigue serves as the primary result of prolonged broken silence in systems. By adhering to rigorous noise control protocols, facilities protect their personnel from hearing loss while simultaneously extending the mean time between failures for their critical valve assets.
Identifying the Technical Causes of Excessive Valve Noise
Acoustic energy in industrial valve systems originates from three distinct physical phenomena. When a system experiences a brokensilenze, or a failure in noise suppression, it typically indicates a deviation from the intended process parameters. Engineers must distinguish between mechanical, aerodynamic, and hydrodynamic sources to implement effective remediation. It’s critical to understand that failure to address these acoustic signals often precedes structural degradation or total component failure within high-pressure environments. Noise isn’t just an environmental concern; it’s a diagnostic indicator of internal stress.
Mechanical Resonance and Stem Vibration
Mechanical noise occurs when the flow frequency aligns with the natural frequency of the valve internal components. This resonance causes lateral stem movement and disc oscillation. If the clearance doesn’t fall within the tight 0.005-inch range required for specific high-flow applications, the resulting clattering sound signifies rapid guide wear. Precision machining to ISO 9001 standards is mandatory to maintain the tolerances required to prevent this instability. Misaligned discs create uneven pressure distributions, leading to fatigue that can result in catastrophic stem failure during 2,500-hour operational cycles.
High-Velocity Gas and Steam Aerodynamics
Aerodynamic noise is the primary concern in gas and steam services where pressure drops exceed 50% of the inlet pressure. As the fluid passes through the vena contracta, it reaches sonic velocity, creating shockwaves and high-frequency turbulence. This transition from laminar to turbulent flow generates sound levels that frequently exceed 110 dBA. Selecting material grades like F11 or F22 forged steel ensures the valve body withstands the erosive forces of these high-velocity flows. Utilizing engineered trim solutions allows for the staged reduction of pressure, effectively mitigating the kinetic energy before it converts into acoustic energy.
Hydrodynamic noise arises from the physics of liquid flow through restricted orifices. In these scenarios, the static pressure drops below the fluid’s vapor pressure, causing the formation of vapor bubbles. The subsequent collapse of these bubbles near the valve wall generates localized pressure spikes reaching 100,000 psi. Industry data suggests that 15% of valve failures in water treatment plants stem from unmanaged cavitation noise. Case studies from offshore platforms show that improper valve selection, specifically choosing a standard globe valve for a high-pressure bypass service, resulted in acoustic failure within 48 hours of commissioning. Adherence to ISA 75.17 standards for noise prediction remains the only reliable method to ensure long-term mechanical integrity. Identifying a brokensilenze event early through acoustic monitoring can prevent the erosion of valve seats and the subsequent loss of shut-off capability.
Cavitation vs. Flashing: Comparing High-Velocity Noise Patterns
Engineers must distinguish between cavitation and flashing to prevent rapid component failure and maintain system uptime. While both phenomena involve phase changes in liquid service, their acoustic signatures and mechanical consequences differ significantly. Cavitation occurs when the liquid pressure drops below the vapor pressure at the vena contracta then recovers. This causes vapor bubbles to collapse violently against the valve internal surfaces. The resulting sound mimics gravel or stones passing through the pipe at high velocity. In severe industrial applications, this noise creates a brokensilenze where sharp, erratic cracks disrupt the steady operational hum, signaling immediate metallurgical distress.
Flashing presents a contrasting acoustic profile. It creates a constant, high-velocity hiss because the downstream pressure remains below the vapor pressure, preventing bubble collapse. The physical damage also varies: cavitation produces localized, cinder-like pitting, while flashing results in smooth, sandblasted erosion patterns. Technical criteria for selecting anti-cavitation valve trims depend on the cavitation index (Sigma). When Sigma values fall below 0.2, multi-stage trims are mandatory to manage the pressure drop in controlled increments.
The Mechanics of Cavitation in Liquid Service
The destructive force of cavitation stems from micro-jets produced during bubble implosion. These jets hit metal surfaces with localized pressures exceeding 100,000 PSI (689 MPa). It’s this mechanical bombardment that leads to the brokensilenze of sharp, metallic cracks often heard in high-pressure water treatment or boiler feed systems. To resist this impact, OG Valves specifies hardened materials for trim components. We utilize Stellite 6 overlays or 440C stainless steel heat-treated to 55-60 HRC. These alloys provide the necessary hardness to withstand the fatigue cycles caused by billions of micro-implosions occurring every second.
Flashing and Downstream Erosion
Flashing occurs when the fluid exits the valve as a two-phase mixture of liquid and vapor. This phenomenon significantly increases the total volumetric flow rate, leading to high-velocity impingement on the valve body and downstream piping. Proper selection of industrial valves for flashing service requires chrome-moly alloys like WC9 or C12A to resist material loss. Design considerations include:
Specifying expanded outlet bodies to accommodate increased vapor volume.
Utilizing angle valve configurations to direct the two-phase flow away from the body wall.
Ensuring exit velocities stay below 150 feet per second to protect downstream piping integrity.
Adhering to ASME B16.34 standards for pressure-temperature ratings during phase transitions.
Maintaining system integrity during flashing requires a clinical focus on material grades and flow geometry. Failure to account for the increased volume often leads to pipe wall thinning and eventual catastrophic rupture in high-energy piping systems.
Engineering Strategies to Mitigate Acoustic Vibration and Fatigue
Acoustic mitigation in high-pressure systems necessitates a shift from standard ball valves to globe valves when pressure ratios exceed 1.8 to 1. Globe valves allow for the integration of tortuous path trims that manage fluid velocity with precision. Maintaining the structural integrity of these systems is vital to prevent a brokensilenze scenario where acoustic energy converts into destructive mechanical vibration. Implementing multi-stage pressure reduction ensures that the total pressure drop is distributed across several stages, keeping the fluid velocity below Mach 0.3 within the valve body. This methodical reduction prevents the fluid from reaching sonic velocity at the vena contracta, which is the primary cause of aerodynamic noise in gas service.
Downstream energy management requires the installation of silencers and diffusers when trim-level attenuation is insufficient. These components function by shifting the frequency of the noise to a range that the piping can more effectively dampen. Engineers should implement regular maintenance protocols, including ultrasonic leak detection and spectral analysis, to ensure the system remains within its original noise specification. These inspections ensure that the silence within the piping remains unbroken, preventing the 15% to 20% increase in noise levels that typically precedes catastrophic trim erosion or seat failure.
Trim Selection for Noise Attenuation
Specialized trims utilize labyrinth paths or multi-stage drilled hole plates to dissipate kinetic energy through friction and controlled directional changes. These designs effectively manage the pressure recovery factor to avoid cavitation in liquid service and choked flow in gas applications. For systems involving low pressure drops and high flow volumes, butterfly valve configurations provide a compact and efficient solution. Accurate calculation of the required Cv is mandatory; sizing a valve to operate between 20% and 80% of its stroke prevents the turbulence associated with throttling near the seat. This precision avoids the brokensilenze of a failing control loop where noise signals impending component fatigue.
Piping Layout and Structural Support
The physical characteristics of the piping network determine the rate of acoustic transmission. Increasing pipe wall thickness from Schedule 40 to Schedule 80 provides a measurable 5 to 7 decibel reduction in radiated noise. Rigid anchoring at intervals defined by ASME B31.3 standards prevents sympathetic vibrations that lead to weld failures and support degradation. Engineers must also calibrate actuator sensitivity to eliminate hunting. Unstable oscillations in the control loop cause rapid pressure fluctuations, which accelerate the wear of internal seals and packing. A stable, well-supported system ensures long-term compliance with ISO 15664 noise control standards.
High-Specification Valve Solutions for Critical Noise Control
Industrial noise mitigation requires more than generic hardware; it demands precise technical procurement and a deep understanding of fluid dynamics. OG Valves utilizes a rigorous specification framework to ensure every component meets the acoustic and mechanical requirements of high-pressure environments. Addressing the phenomenon of brokensilenze requires valves that maintain structural integrity under extreme turbulence and cavitation. We prioritize engineering excellence over standard shelf-ready solutions, focusing on the quantifiable performance of every unit. Our approach centers on identifying the exact mechanical stressors that lead to acoustic failure, ensuring that replacement components exceed the original design life of the system.
Technical Consultation and Material Integrity
Engineers often face complex challenges when selecting components for severe service applications. OG Valves provides comprehensive support to help technical teams specify the correct gate valve for isolation purposes. This process includes the provision of technical data sheets that detail acoustic performance and flow coefficients. Every high-pressure component undergoes Positive Material Identification (PMI) testing to verify alloy grades. This ensures that the material integrity matches the project’s chemical and thermal requirements, preventing premature fatigue and the onset of brokensilenze within the pipeline architecture. We provide detailed material test reports (MTRs) to confirm that every forged or cast body meets the specified metallurgical standards.
Global Logistics for Minimal Downtime
The financial impact of system failure extends far beyond the cost of the hardware itself. Rapid response is mandatory for critical infrastructure in the oil, gas, and water treatment sectors. OG Valves manages complex, multi-valve projects through a streamlined global supply chain designed for speed and reliability. Fast-track delivery protocols ensure that failed valves are replaced within optimized timeframes, directly minimizing the secondary costs associated with unplanned outages. Our inventory and production schedules are strictly aligned with international safety benchmarks to ensure immediate compliance upon installation.
Compliance: All components adhere strictly to API 6D for pipeline valves and ASME B16.34 for pressure-temperature ratings.
Testing: Every valve is subjected to rigorous hydro-testing and gas-testing procedures prior to dispatch.
Integrity: We utilize advanced sealing technologies to prevent fugitive emissions and maintain system vacuum or pressure.
Our technical team is available to conduct a detailed specification review for your upcoming project. By analyzing the specific acoustic and mechanical demands of your facility, we provide a tailored procurement roadmap that eliminates the risks of premature component failure. Contact our engineers today to ensure your infrastructure meets the highest standards of industrial precision and safety.
Achieving Operational Stability through Advanced Acoustic Diagnostics
Effective management of high-velocity noise patterns like cavitation and flashing is essential for maintaining the structural integrity of industrial piping. These acoustic phenomena indicate underlying mechanical stress that leads to rapid component degradation. Identifying a state of brokensilenze within these systems allows engineers to implement targeted trim modifications before vibration-induced fatigue compromises safety. Adherence to ASME B16.34 and API 6D standards ensures that every valve assembly withstands the rigorous demands of high-pressure service environments. It’s vital to prioritize durability over temporary fixes to secure long-term performance.
Since 2014, OG Valves has focused on high-specification industrial supply for the oil, gas, and water treatment sectors. Our commitment to engineering excellence is backed by global fast-track delivery capabilities and strict compliance with ISO 9001 quality management protocols. We provide the technical expertise needed to diagnose complex failure modes and deliver precision-engineered solutions that meet exact project requirements. Reliability isn’t just a goal; it’s a measurable outcome of rigorous testing and material selection.
Investing in high-specification components today ensures a safer and more efficient industrial future.
Frequently Asked Questions
What is the primary cause of noise in industrial control valves?
Aerodynamic noise resulting from high velocity gas or vapor flow remains the primary cause of industrial valve noise. According to the IEC 60534-8-3 standard, this occurs when fluid velocity exceeds Mach 0.3 at the valve trim. The resulting turbulence generates pressure fluctuations that manifest as high frequency sound. Engineers must monitor these levels to prevent structural fatigue in piping systems during high pressure operations.
How can I distinguish between cavitation and mechanical vibration noise?
Cavitation produces a distinct rattling sound similar to gravel flowing through the pipe, while mechanical vibration manifests as a consistent resonance or hum. Cavitation occurs when local pressure drops below the fluid’s vapor pressure, leading to bubble collapse at forces exceeding 100,000 PSI. Mechanical vibration results from lateral movement of the valve plug at frequencies between 500 Hz and 2,000 Hz, often caused by fluid-induced excitation.
Is valve noise always a sign of imminent component failure?
Noise isn’t always an indicator of immediate failure, but levels exceeding 85 dBA require immediate technical evaluation. The OSHA 1910.95 standard dictates that exposure to such decibel levels over an 8-hour shift necessitates hearing protection. Sustained noise at 110 dBA can lead to trim erosion and seal degradation within 500 operating hours. It’s a critical diagnostic signal that engineers shouldn’t ignore if they want to maintain system integrity.
What are the industry standards for measuring valve noise levels?
The IEC 60534-8-4 standard provides the definitive framework for measuring and predicting aerodynamic noise in control valves. Technicians perform these measurements at a distance of 1 meter downstream from the valve body and 1 meter from the pipe surface. This protocol ensures data consistency across global industrial sites, adhering to ISO 9001 quality management requirements. Accurate measurement is the first step in addressing a brokensilenze in a pressurized environment.
Can a check valve cause a ‘broken silence’ through water hammer?
A check valve causes a brokensilenze through water hammer when the disc slams shut during a sudden flow reversal. This event generates pressure spikes that reach 200% of the normal operating pressure in less than 0.1 seconds. These surges create a loud, metallic bang that signals potential damage to gaskets and pipe supports. Proper selection of non-slam check valves with closure times under 0.5 seconds effectively mitigates this risk.
How do multi-stage trims reduce aerodynamic noise in steam valves?
Multi-stage trims reduce aerodynamic noise by distributing the total pressure drop across several discrete stages to keep velocities below sonic levels. Each stage manages a fraction of the pressure, preventing the fluid from reaching its critical pressure ratio. This engineering approach effectively lowers noise output by 20 to 35 dBA compared to standard single-stage designs. It’s a proven method for maintaining compliance with noise pollution regulations in steam power plants.
What materials are best suited for high-noise, high-pressure environments?
When should a silencer be used instead of an anti-noise valve trim?
Use an anti-noise valve trim when you need to prevent noise generation at the source, whereas silencers are appropriate for treating noise that has already developed downstream. Anti-noise trims can achieve a 30 dBA reduction in sound pressure levels by managing fluid energy. Silencers are typically utilized in vent applications where downstream attenuation of 15 to 25 dBA is required to meet local environmental regulations without modifying the internal valve architecture.
 Responsive Menu