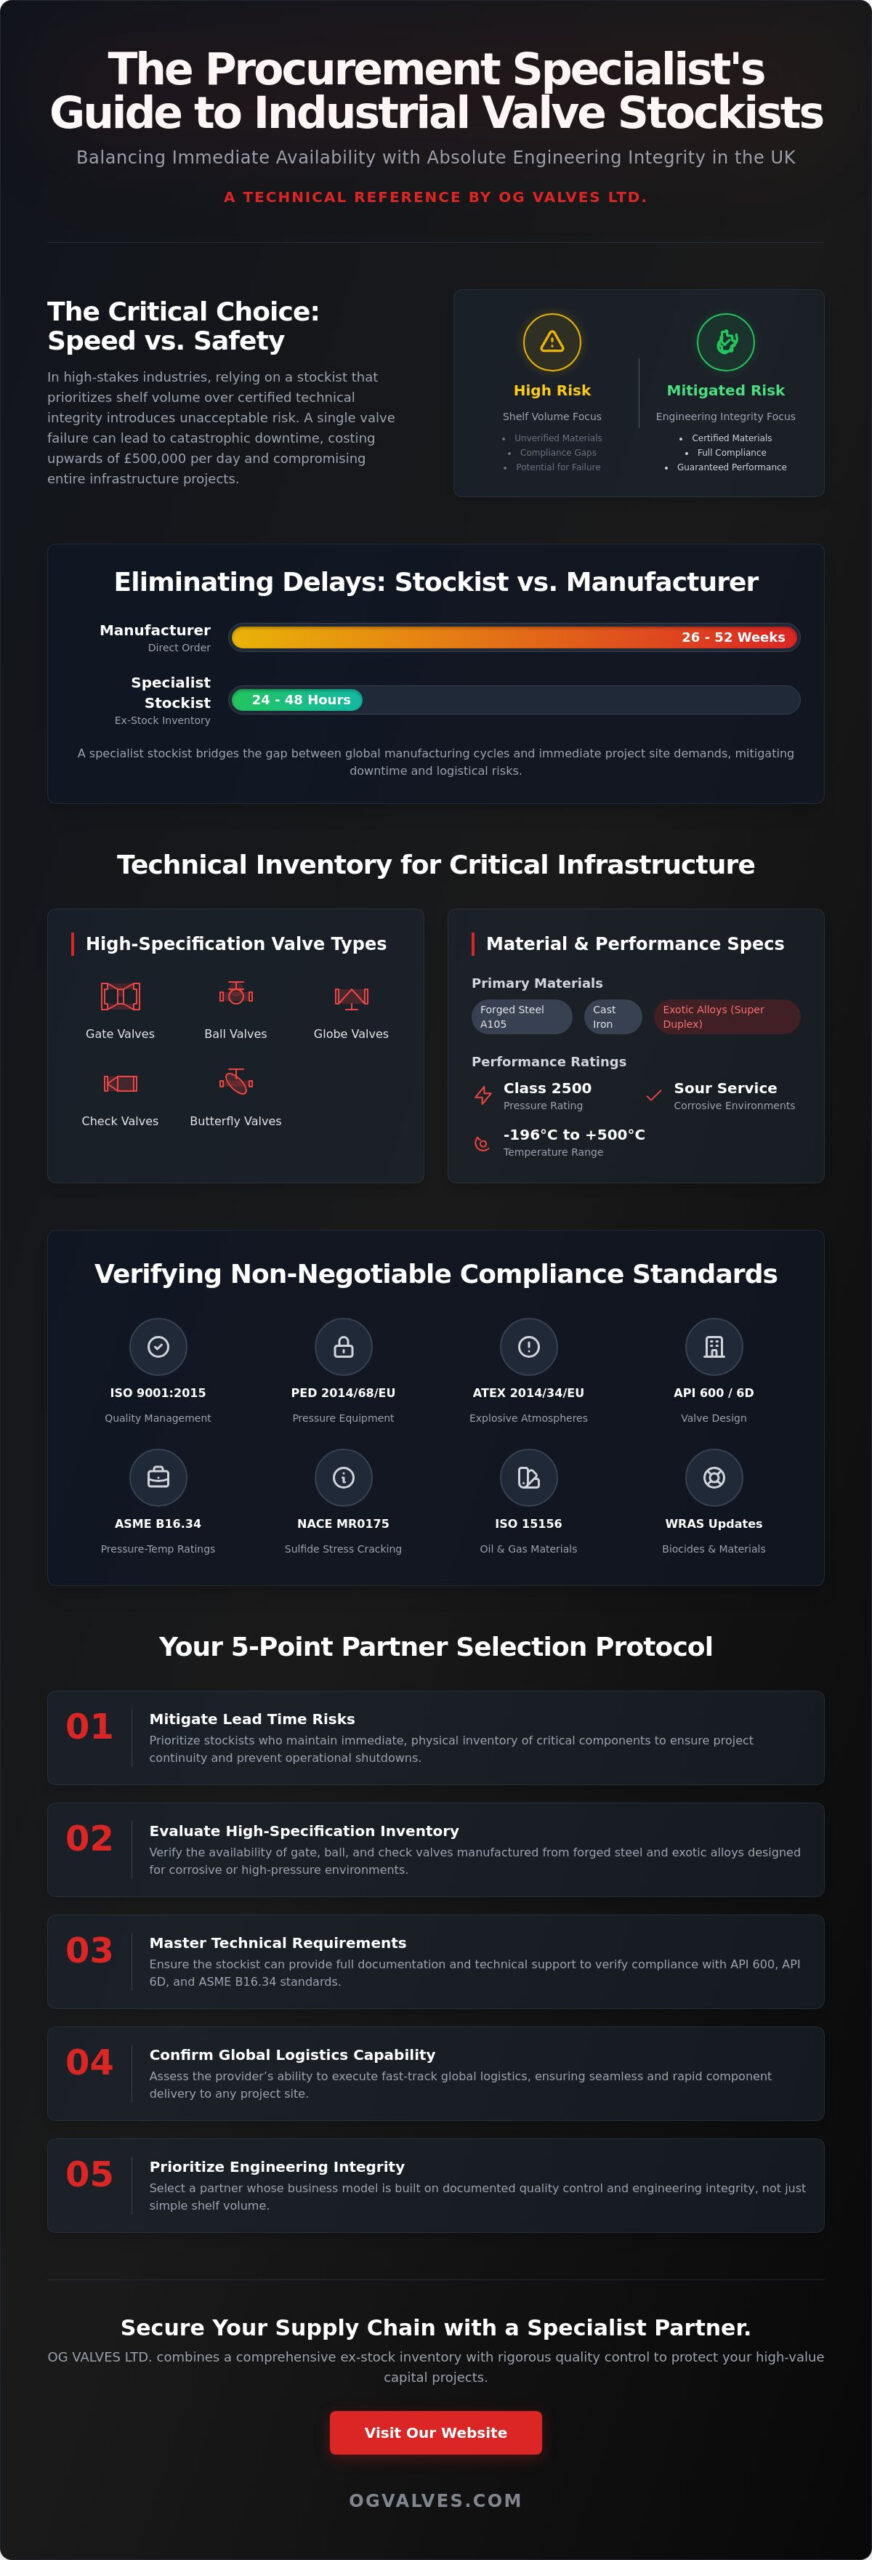
What if your primary industrial valve stockist in the United Kingdom is prioritizing shelf volume over the technical integrity required for sour service? In high-pressure environments, the cost of a valve failure far exceeds the initial procurement price. You understand that while rapid delivery is essential to avoid operational downtime, material non-compliance remains a critical risk. Relying on components that lack verified NACE MR0175 or ISO 15156 certification can compromise the safety of entire infrastructure projects in the oil and gas sectors.
This technical reference provides procurement specialists with a framework to select a stockist that balances immediate inventory availability with absolute engineering compliance. You’ll learn how to verify that gate, ball, and check valves meet the latest PED 2014/68/EU and ATEX 2014/34/EU directives. We also examine the implications of the November 2024 WRAS regulation updates regarding biocides and material testing. This guide details the rigorous quality management protocols, including ISO 9001:2015 standards, necessary to ensure your high-value capital projects proceed without technical friction or material failure.
Key Takeaways
- Identify how a specialized industrial valve stockist united kingdom mitigates lead time risks by maintaining immediate inventory for critical energy and process infrastructure.
- Evaluate high-specification valve types including gate, ball, and check valves manufactured from forged steel and exotic alloys to ensure durability in corrosive environments.
- Master the technical requirements of API 600, API 6D, and ASME B16.34 to verify that all components meet rigorous pressure-temperature ratings and safety certifications.
- Implement fast-track global logistics strategies to prevent operational shutdowns and ensure seamless component delivery for large-scale capital projects.
- Establish a selection protocol for a procurement partner that prioritizes engineering integrity and documented quality control over simple shelf volume.
The Strategic Role of an Industrial Valve Stockist in the United Kingdom
An industrial valves stockist represents a vital node within the global energy and process supply chain. While manufacturers prioritize long-term production cycles and high-volume orders, the industrial valve stockist united kingdom focuses on immediate availability and project agility. This distinction is critical for national infrastructure projects where a delay in component arrival can halt multi-million pound operations. Manufacturers often cite lead times of 26 to 52 weeks for custom-forged components. A specialist stockist eliminates this lag by holding physical inventory of gate, ball, and check valves. This UK-based inventory reduces logistical risks associated with international shipping and customs delays, ensuring that critical components are available for immediate dispatch.
An industrial valve stockist acts as a technical buffer against industrial downtime by maintaining immediate access to high-specification components that meet rigorous compliance standards. By maintaining a localized inventory, these entities provide a safeguard against the volatility of global manufacturing schedules and raw material shortages.
Mitigating Downtime through Immediate Availability
Unplanned maintenance in the petrochemical and power sectors can cost operators upwards of £500,000 per day in lost production. In these high-stakes environments, “ex-stock” status is the primary KPI for procurement specialists. Stockists support fast-track maintenance, repair, and operations (MRO) by providing components that have already cleared initial quality assurance phases. This readiness ensures that critical infrastructure remains functional even when sudden component failure occurs. The ability to source a replacement valve within 24 to 48 hours is often the difference between a minor service interruption and a catastrophic operational shutdown.
Bridging the Gap Between Global Manufacturers and Local Sites
Procuring high-specification components from global manufacturers involves navigating complex lead times and varying international standards. A specialist stockist simplifies this by consolidating components that adhere to PED 2014/68/EU and ATEX 2014/34/EU directives. Technical support during the selection process is indispensable. Engineers rely on the stockist’s expertise to ensure material grades, such as forged steel or exotic alloys for sour service, match the specific corrosive or high-pressure demands of the site. This technical oversight reduces procurement friction and ensures that every valve delivered is fit for its intended industrial purpose.
- Reduces lead times from months to days for critical MRO requirements.
- Ensures compliance with ISO 9001:2015 quality management systems before the product reaches the site.
- Provides a localized point of contact for technical validation and material certification.
Technical Inventory: High-Specification Valves for Critical Infrastructure
A proficient industrial valve stockist united kingdom must maintain a technical inventory that exceeds standard commercial grades. Critical infrastructure requires components capable of withstanding extreme pressure and highly corrosive environments. Engineering selection frameworks for industrial valves prioritize material integrity, specifically focusing on forged steel A105, cast iron, and exotic alloys like Super Duplex for offshore applications. These material choices align with the UK government’s focus on Strategic Supply Chain Management to ensure long-term resilience in national energy and manufacturing sectors. Technical specifications must account for pressure ratings up to Class 2500 and temperature ranges extending from cryogenic service at -196°C to high-temperature steam applications exceeding 500°C.
Inventory availability is categorized by functional requirement, encompassing gate, ball, globe, check, and butterfly designs. Each valve type serves a specific role within the process loop, from isolation to non-return safety. For projects involving sour service, components must adhere to NACE MR0175/ISO 15156 standards to prevent sulfide stress cracking. Procurement specialists should verify that stockists provide full material traceability, including Mill Test Reports (MTRs) for every high-specification component. If you require immediate technical validation for your project, you can view our full range of certified components.
Isolation and Control: Ball and Butterfly Valve Specifications
Engineers distinguish between floating and trunnion-mounted ball valves based on the required sealing force and torque limits. In high-pressure isolation scenarios above Class 600, trunnion-mounted designs are mandatory to manage seat load effectively. For power generation and large-scale water treatment, triple offset butterfly valves provide zero-leakage performance. These valves utilize a non-rubbing design that minimizes wear in high-cycle applications. Material selection for abrasive slurries often dictates the use of hardened trim or ceramic linings to ensure component longevity in chemical processing environments.
Specialist Components: Plug and Needle Valves
Precision flow regulation in instrumentation loops necessitates the use of high-pressure needle valves. These components allow for fine adjustment of flow rates in auxiliary lines and sampling systems. In contrast, plug valves are selected for their durability in wastewater and oil-and-gas sectors, particularly when handling fluids with high solid content. Their robust seating surfaces offer superior resistance to erosion compared to standard gate valves. Sizing considerations for these auxiliary valves are critical; improper specification can lead to localized pressure drops that compromise the integrity of the entire instrumentation system.
- Forged steel and super duplex alloys for high-pressure isolation.
- Triple offset designs for zero-leakage in high-temperature steam.
- Needle and plug valves for precision regulation and slurry handling.
Rigorous Compliance: Understanding API, ASME, and ISO Certification Standards
Rigorous adherence to international standards isn’t optional for an industrial valve stockist united kingdom operating in high-pressure sectors. Compliance serves as the primary barrier to catastrophic material failure in volatile environments. Engineering specifications for steel gate valves must align with API 600, which dictates wall thickness and stem diameter requirements to ensure long-term durability. For pipeline applications, API 6D remains the mandatory standard for ball and check valves, specifying the design, manufacturing, and testing protocols. These standards ensure that every component integrated into a critical process loop can withstand the intended service conditions without compromising system integrity.
ASME B16.34 provides the essential requirements for pressure-temperature ratings, which engineers use to determine the safe operating limits of a valve body. Quality management systems, often verified through the British Standards Institution (BSI), provide the framework for ISO 9001:2015 certification. This certification ensures that the stockist maintains consistent product integrity throughout the procurement and storage lifecycle. Without these documented standards, the risk of material non-compliance in corrosive or high-temperature environments increases significantly, potentially leading to expensive project delays or safety breaches.
Material Traceability and PMI Testing
Positive Material Identification (PMI) is a critical verification step for an industrial valve stockist united kingdom. It uses X-ray fluorescence (XRF) to confirm the chemical composition of alloys, ensuring that a valve marked as 316 Stainless Steel or Super Duplex actually meets those specific metallurgical requirements. Material traceability is documented via EN 10204 certification. While 3.1 certification is standard for manufacturer-verified products, 3.2 certification involves independent third-party inspection, which is often mandatory for high-risk offshore service. Non-destructive testing (NDT), including ultrasonic and dye penetrant inspections, further validates that the valve body is free from internal defects or surface cracks.
Fire Safe and Low Emission Standards
Hazardous areas require valves that maintain their seal even during a thermal event. API 607 compliance confirms that ball or butterfly valves have passed rigorous testing under fire conditions, preventing the leakage of flammable media. Environmental regulations also demand a focus on fugitive emissions. ISO 15848-1 certified valve packing is designed to minimize the release of volatile organic compounds (VOCs) into the atmosphere. These certifications are increasingly specified in the UK to align with strict environmental performance targets, ensuring that infrastructure remains compliant with both safety and ecological mandates.
- API 600 and API 6D for standardized design and pipeline safety.
- PMI testing and EN 10204 3.2 for absolute material traceability.
- ISO 15848-1 and API 607 for environmental and fire safety compliance.
Strategic Supply Chain Management and Fast-Track Global Logistics
Managing the procurement cycle for multi-million pound capital projects requires more than simple warehousing; it demands a sophisticated logistical framework. An industrial valve stockist united kingdom acts as a central hub for the movement of high-specification components across international borders. Fast-track delivery is a critical mechanism for preventing operational shutdowns that can cost operators upwards of £500,000 per day in the petrochemical sector. Global distribution necessitates rigorous attention to customs compliance and the provision of localized export documentation to ensure seamless transit through international ports. This logistical precision ensures that critical infrastructure projects remain on schedule regardless of geographical constraints.
Efficiency in global logistics depends on the stockist’s ability to consolidate complex valve packages for immediate dispatch. For instance, a major industrial project might require a combination of gate, ball, and check valves, all with specific material certifications. By centralizing this inventory within the UK, the stockist reduces the administrative burden on the end-user. This centralized approach ensures that all components arrive at the site simultaneously, accompanied by the necessary regulatory filings and safety certifications. It eliminates the risk of project delays caused by fragmented supply chains or uncoordinated shipping schedules.
Project Management and Documentation
Successful engineering handovers rely on comprehensive data packages that document every stage of the procurement process. Project management involves tracking every component from the foundry to the final installation site. Strategic inventory forecasting uses historical demand data to anticipate the needs of major infrastructure upgrades, ensuring that lead times remain minimal even during periods of global material scarcity. Documentation sets typically include Mill Test Reports (MTRs), pressure test certificates, and compliance declarations for PED 2014/68/EU. These records are essential for maintaining the technical audit trail required by safety regulators and insurance underwriters.
Technical Support and After-Sales Service
Procurement specialists require access to engineering expertise to validate valve sizing and material selection before an order is finalized. Technical data sheets and high-resolution CAD drawings are essential for integrating valves into complex piping designs without error. A professional industrial valve stockist united kingdom provides these resources to eliminate ambiguity during the design phase. Managing warranty and replacement cycles ensures long-term performance and reliability of the critical infrastructure. If your project requires immediate logistical coordination and technical validation, request a technical consultation with our sales team.
- Consolidated shipping of complex valve packages to reduce site-side administrative costs.
- Provision of full documentation sets, including MTRs and PED compliance certificates.
- Strategic forecasting to maintain ex-stock availability for high-demand components.
Selecting OG VALVES LTD. as Your Specialist Industrial Procurement Partner
OG VALVES LTD. functions as a seasoned industrial expert, prioritizing technical precision over commercial volume. As a primary industrial valve stockist united kingdom, the business provides the engineering validation required for high-stakes trust in the energy and process sectors. The brand presents itself as an established global entity that acts as a dependable partner in critical infrastructure safety rather than a mere vendor. This positioning is supported by a clinical focus on durability and unwavering compliance with international standards such as ASME, API, and ISO. High-stakes industrial sectors, including oil, gas, and water treatment, require a partner that understands the severe cost of component failure and the necessity of quality.
The strategic advantage of selecting OG VALVES LTD. lies in the synthesis of global supply chain reach and deep technical expertise. Procurement specialists benefit from a methodical approach to supply that ensures all technical data is communicated without ambiguity. This eliminates the risk of material non-compliance in corrosive or high-pressure environments. The organization’s commitment to industrial precision ensures that all products, from forged steel gate valves to cryogenic ball valves, meet the exact specifications required for heavy industry applications. Every claim is anchored in rigorous testing and quality control processes, positioning the name as a benchmark for industrial safety.
Specialised Inventory for High-Stakes Environments
Inventory management focuses on high-specification gate, globe, ball, and check valves specifically engineered for the oil, gas, and power generation sectors. Reliability is maintained through a robust supply chain that supports fast-track delivery, minimizing the risk of operational downtime during critical maintenance cycles. The technical team at OG VALVES LTD. provides direct support for complex engineering requirements, assisting with material selection for exotic alloys and high-pressure service. This technical validation ensures that every valve delivered is fit for its intended purpose and adheres to the latest PED and ATEX directives. Our focus remains on functional reality and long-term performance above all else.
Request a Technical Specification or Quote
The RFQ process is designed to accommodate the complexity of large-scale industrial valve packages without unnecessary administrative friction. Procurement teams can access a comprehensive technical documentation and certification library, including Mill Test Reports (MTRs) and detailed CAD drawings. This transparency ensures that technical audits and safety reviews are conducted with complete data sets and zero ambiguity. Streamlining the quotation process allows for rapid response times, ensuring that project timelines remain intact even during urgent MRO phases. To secure high-specification components for your next infrastructure project, you can contact our technical sales team for your industrial valve requirements.
- Specialist focus on high-specification components for oil, gas, and power sectors.
- Technical validation provided by a seasoned engineering team for every RFQ.
- Rigorous adherence to international certifications including API, ASME, and ISO standards.
Securing Technical Integrity for Future Infrastructure
Maintaining the operational safety of critical infrastructure in 2026 requires a transition from transactional procurement to high-specification technical partnership. A reliable industrial valve stockist united kingdom must provide more than physical inventory; it must deliver documented engineering compliance. You’ve identified how adherence to API 600 and ASME B16.34 standards serves as the primary defense against material failure in corrosive or high-pressure environments. Ensuring material traceability through PMI testing and EN 10204 3.1 certification is essential for long-term asset integrity and regulatory alignment.
OG VALVES LTD. supports your project requirements with an ASME and API compliant inventory and specialist technical engineering support. Our global logistics and fast-track delivery capabilities ensure that lead times don’t compromise your operational schedule. By prioritizing clinical precision and rigorous quality control, we act as a dependable partner for the heavy industry sector. You can request a technical quote for high-specification industrial valves to begin your procurement process. We look forward to supporting your engineering objectives with the precision your infrastructure demands.
Frequently Asked Questions
What is the role of an industrial valve stockist in the United Kingdom?
An industrial valve stockist united kingdom manages technical risk by ensuring that high-specification components are available for immediate deployment. This localized inventory prevents the severe delays associated with international manufacturing cycles. It’s a strategic buffer for critical infrastructure, allowing operators to maintain system uptime during both planned maintenance and emergency repair scenarios.
How do you verify the material integrity of valves in your stock?
We verify material integrity through documented traceability and rigorous metallurgical testing. Every valve is cross-referenced with its Mill Test Report to confirm adherence to the specific material grade required for the service environment. This process ensures that components intended for corrosive or high-pressure applications meet the precise chemical and physical properties defined in the project specification.
Can OG VALVES LTD. provide fast-track delivery to international industrial sites?
OG VALVES LTD. utilizes a sophisticated global logistics network to facilitate the fast-track delivery of valve packages to international sites. Our logistical framework manages export compliance and documentation to ensure seamless transit across borders. This capability is essential for multi-site industrial operations that require synchronized component delivery to maintain project timelines.
Which international standards do your industrial valves comply with?
Our inventory complies with established international benchmarks including API 600, API 6D, and ASME B16.34. These standards define the design and pressure-temperature ratings necessary for industrial safety. As an industrial valve stockist united kingdom, we ensure that all components also meet ISO 9001:2015 quality management requirements to guarantee consistent performance across our entire product range.
What happens if a valve fails in a high-pressure corrosive environment?
Valve failure in high-pressure environments can result in catastrophic operational loss and safety breaches. Using non-compliant materials in sour service increases the risk of sulfide stress cracking and localized erosion. To mitigate this, we provide components that don’t compromise the mechanical integrity of the process loop under aggressive conditions.
Do you provide technical support for valve sizing and material selection?
OG VALVES LTD. provides comprehensive technical support to assist procurement specialists with valve sizing and material selection. Our engineering expertise ensures that components are correctly specified for their intended pressure and temperature ranges. This technical validation reduces the likelihood of procurement errors and enhances the long-term reliability of the infrastructure.
What types of industrial valves are available for immediate dispatch?
We maintain a technical inventory of gate, globe, ball, check, and butterfly valves for immediate dispatch. Auxiliary components including plug and needle valves are also available to support precision instrumentation needs. These valves are stocked in various material grades, such as forged steel and cast iron, to support diverse industrial requirements.
Is PMI testing included as part of your quality assurance protocol?
PMI testing is a standard component of our quality assurance protocol for all high-specification alloys. This testing confirms the metallurgical composition of the valve body and trim before it is released for dispatch. By verifying the alloy grade through X-ray fluorescence, we provide absolute assurance that the component meets the rigorous demands of the industrial application.
 Responsive Menu