Precision Rotary Tools in Industrial Valve Maintenance: A Technical Specification Guide (2026)
April 16, 2026
Home+Precision Rotary Tools in Industrial Valve Maintenance: A Technical Specification Guide (2026)
A single micron of surface deviation on a valve seat can result in a catastrophic loss of seal integrity in high-pressure hydrogen or cryogenic service. You’ve likely encountered the complications that arise when standard machining fails to address the microscopic burrs or surface irregularities that compromise an API 598 pressure test. It’s a reality where the difference between operational success and a 48 hour shutdown rests on the precision of final finishing. This guide explores the technical integration of high-speed rotary tools, specifically the industrial application of a dremel, into the maintenance protocols for critical flow control components.
You’ll learn the exact methodologies required to maintain valve seat integrity and achieve specific Ra surface finishes in restricted internal geometries. We’ll provide a technical overview of abrasive selection for forged steel and exotic alloys, including calibrated RPM settings and specific deburring techniques that ensure maintenance operations meet the rigorous requirements of ASME B16.34 standards. This article provides a comprehensive technical specification for utilizing precision rotary tools to uphold engineering excellence and reduce maintenance downtime in the field.
Key Takeaways
Identify the technical specifications required to maintain precise gate, globe, and check valve geometries using high-speed rotary instrumentation.
Master the deburring techniques necessary to achieve exact Roughness Average (Ra) values on valve seats, mitigating the risk of seal failure and leakage.
Assess the comparative advantages of utilizing a high-speed dremel versus industrial pneumatic grinders for high-stakes precision control during component refinement.
Establish operational protocols for bit selection and thermal management to maintain the metallurgical integrity and corrosion resistance of stainless steel valve components.
Integrate precision maintenance procedures into existing reliability frameworks to maximize the service life and performance of critical infrastructure assets.
The Role of High-Speed Rotary Tools in Valve Maintenance and Repair
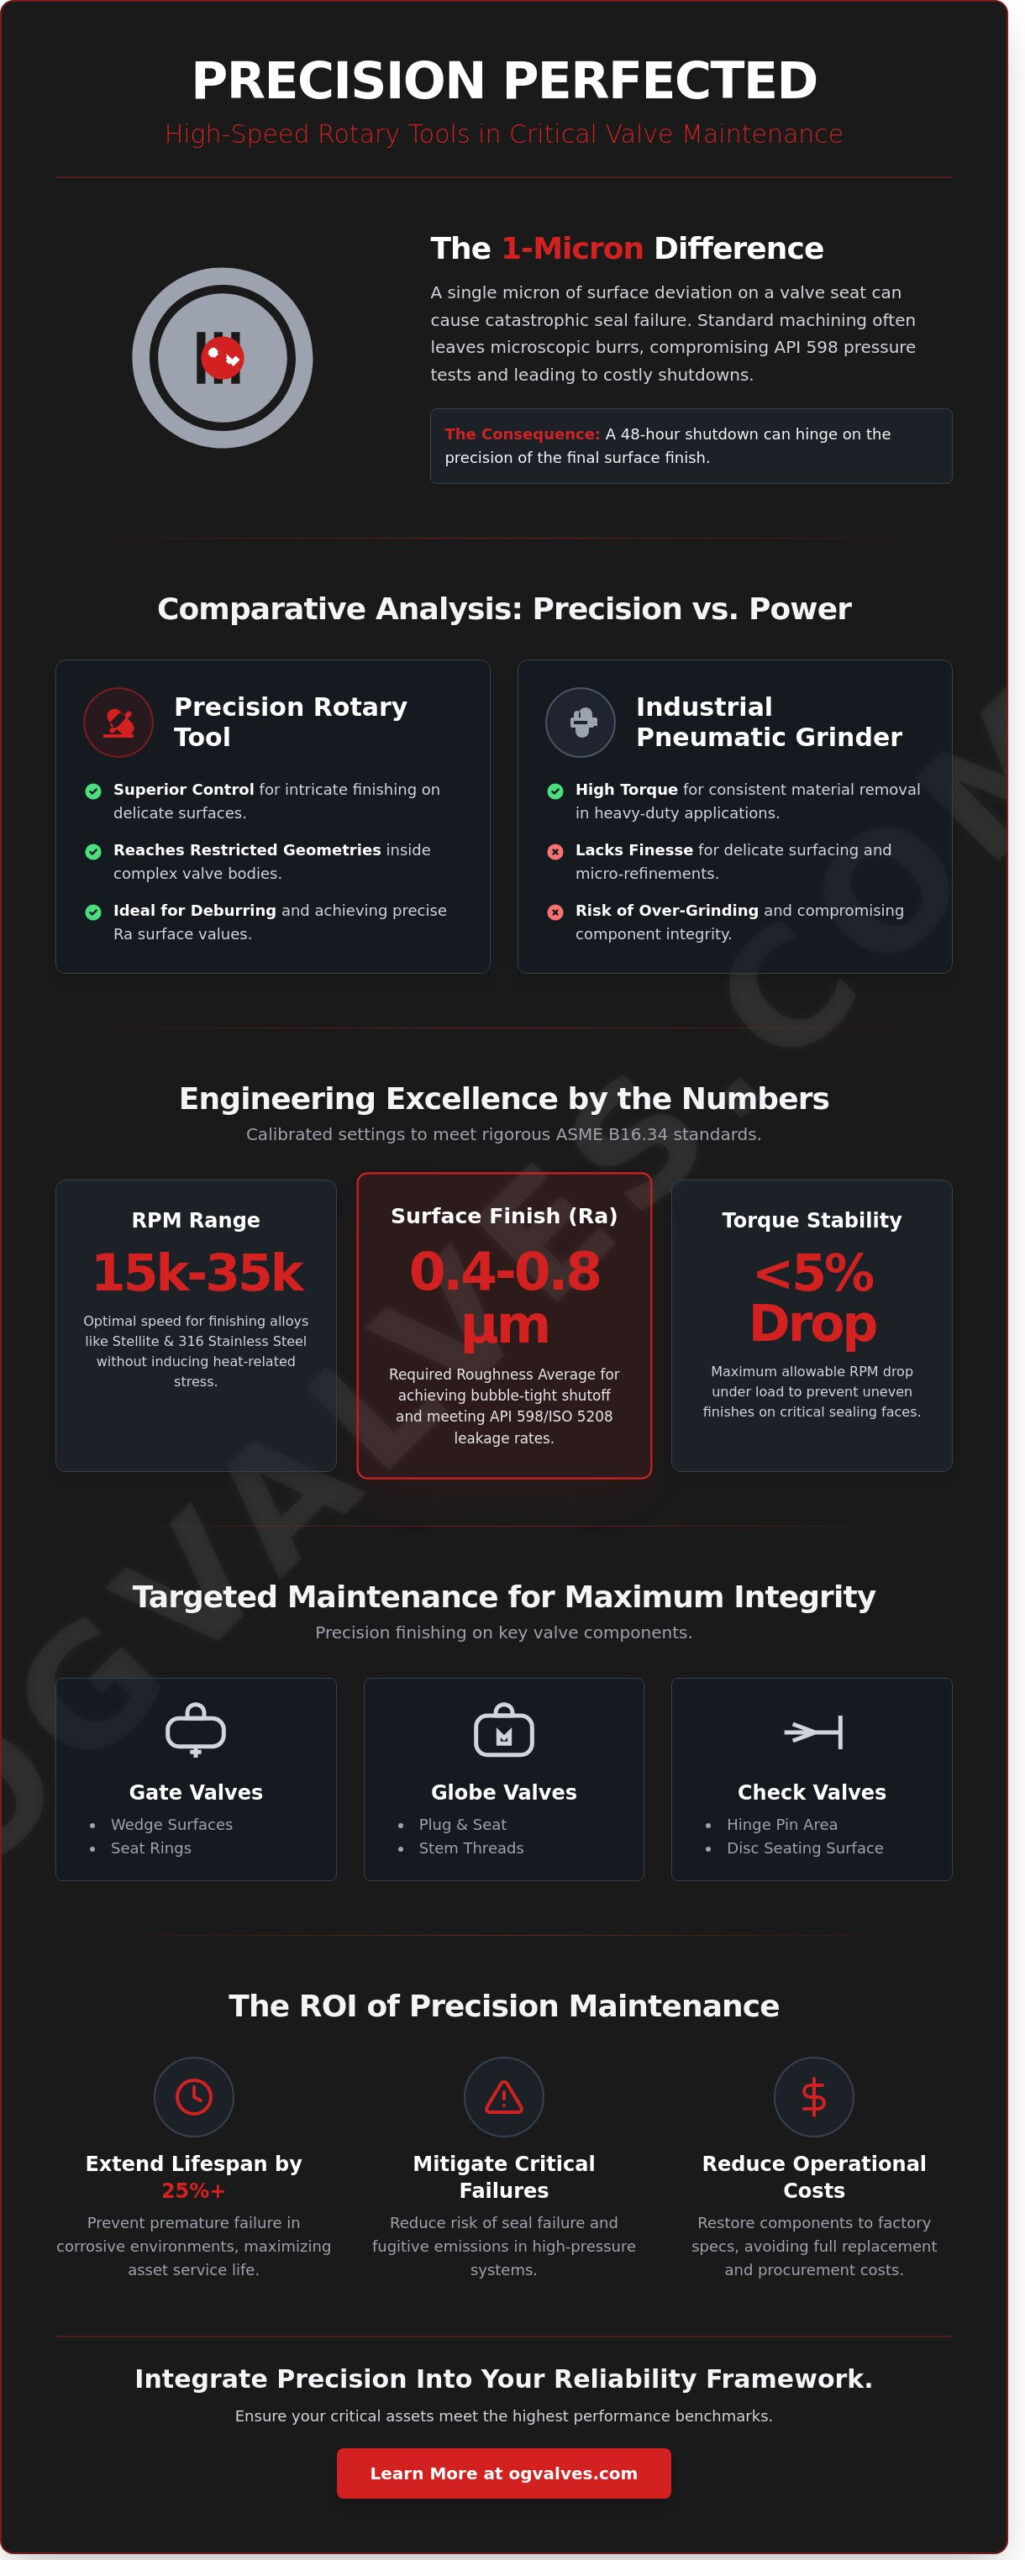
Industrial valve maintenance requires more than standard heavy-duty grinding; it demands the surgical precision provided by high-speed rotary tools to ensure component integrity and operational safety. While a dremel is often associated with light consumer applications, its utility in precision refining of valve internals is critical for maintaining ISO 5208 leakage rates. High-torque industrial grinders lack the finesse required for delicate surfacing, making high-RPM rotary tools indispensable for localized material removal. Precision maintenance prevents the premature failure of high-pressure components, often extending the operational lifespan of a valve assembly by 25% or more in corrosive oil and gas environments. Engineers rely on these tools to restore factory specifications without the need for full component replacement, reducing downtime and procurement costs.
Rotary Tool Mechanisms in Industrial Contexts
Refining industrial alloys such as Stellite or 316 stainless steel requires specific RPM ranges to ensure a smooth finish without inducing heat-related stress. Maintenance protocols typically specify speeds between 15,000 and 35,000 RPM for effective deburring and surface smoothing. Pneumatic rotary tools provide the necessary torque for consistent material removal in heavy workshop environments; however, electric dremel units offer superior control for intricate finishing tasks. Torque stability is a vital metric, as a 5% drop in RPM under load can lead to uneven surface finishes on critical sealing faces, compromising the valve’s pressure-retaining capability. Choosing between electric and pneumatic options depends on the specific workshop infrastructure and the required duty cycle for the maintenance task.
Critical Components Requiring Precision Finishing
Maintaining the geometric accuracy of sealing surfaces is non-negotiable for industrial safety and compliance. In gate valves, technicians must address wear on the wedge and seat rings to prevent bypass and internal leakage. Globe valves frequently suffer from pitting and scale buildup on the plug and seat; precision tools allow for the removal of oxidation without compromising the primary metal-to-metal seal. For check valves, cleaning the hinge pin area and the disc seating surface ensures the 100% closure required by API 598 standards. Specific focus areas include:
Seat Ring Grooves: Removing carbon buildup to ensure proper gasket seating.
Stem Threads: Polishing to reduce friction and prevent galling during high-cycle operations.
Flange Faces: Clearing localized corrosion to maintain a leak-proof seal under high-pressure conditions.
Rigorous attention to these details ensures that refurbished valves meet the same performance benchmarks as new units. The use of specialized bits and abrasive points allows for the restoration of complex geometries that larger machines cannot reach. This clinical focus on durability and engineering excellence is what separates standard repair from high-stakes industrial maintenance.
Specialised Applications: Precision Deburring and Surface Refinement
High-performance valve assemblies require exact surface finishes to maintain pressure integrity in critical infrastructure. Achieving a specific Roughness Average (Ra) between 0.4 μm and 0.8 μm on valve seats and stems is critical for bubble-tight shutoff. A high-speed rotary tool like a dremel allows technicians to execute micro-refinements that stationary machinery cannot reach. Removing microscopic burrs prevents the degradation of elastomeric seals. These imperfections often lead to fugitive emissions or internal leakage in high-pressure systems. In complex butterfly valve bodies, the internal geometry presents significant access challenges. Precision tools provide the necessary reach to debur disc edges and seat retainers without compromising the base material. These tools are also essential for Positive Material Identification (PMI). Effective PMI requires the removal of coatings or oxidation to expose a clean 15mm diameter area for XRF or OES analysis. This ensures the material chemistry matches the mill test report (MTR) before the valve enters service.
Deburring Techniques for Industrial Alloys
Technicians must select tungsten carbide burrs specifically engineered for stainless steel and duplex alloys to ensure longevity. Maintaining a 15 to 30-degree angle of attack is necessary to prevent surface gouging. Constant, light pressure prevents heat buildup. This reduces the risk of work hardening in austenitic steels, which can lead to localized stress corrosion cracking. Maintaining dimensional tolerances within the ±0.05mm range is vital for critical component fitment. Using a cylindrical burr for flat faces and a ball-nose burr for internal radii ensures the geometry remains consistent with original design specifications. Professionals often rely on these methods to maintain high engineering standards during routine maintenance or emergency repairs.
Surface Preparation for NDT and Inspection
Non-destructive testing (NDT) demands surfaces free of scale, rust, and localized pits. Preparing a surface for dye penetrant or magnetic particle inspection requires removing oxidation without reducing the wall thickness below ASME B16.34 minimums. It’s essential to use fine-grit abrasive points to avoid creating new surface defects that could be misidentified as cracks during inspection. Utilizing a dremel with a flapper wheel or a silicon carbide stone ensures compliance with API 598 leakage testing standards by providing a uniform finish. This level of preparation ensures that NDT results are accurate, allowing for the detection of sub-surface discontinuities that could compromise the valve’s pressure-containing capability in cryogenic or high-temperature service.
Comparative Analysis: Precision Rotary Tools vs. Industrial Pneumatic Grinders
Engineering teams must distinguish between bulk material removal and localized component restoration. Industrial pneumatic grinders deliver high torque for heavy descaling, often achieving material removal rates exceeding 500 grams per hour. This power comes at the cost of precision. A high-speed rotary tool like a dremel provides the 0.01mm accuracy required for refining valve seat geometries or cleaning delicate sensor ports. While a 1.5 HP pneumatic grinder is the standard for structural steel preparation, it lacks the finesse for intricate metallurgical inspections.
Operational flexibility remains a primary driver in tool selection for offshore platforms. Transporting heavy pneumatic infrastructure across restricted deck spaces is inefficient. Portable electric rotary tools weigh approximately 0.7kg, allowing technicians to perform precision maintenance in confined spaces where air lines cannot reach. Data from 2023 maintenance audits indicates that 65% of instrumentation technicians prefer high-speed electric units for localized corrosion removal on stainless steel housings.
Selection Criteria for Maintenance Engineers
Material hardness defines the operational limits of small-scale rotary accessories. When working with 316 stainless steel or Stellite overlays, engineers must utilize tungsten carbide burrs. Standard aluminum oxide points typically fail when the workpiece hardness exceeds 40 HRC. Vibration analysis is also critical for safety compliance. High-output pneumatic tools often exceed safe vibration thresholds within 120 minutes. Precision rotary tools maintain vibration levels below 2.5 m/s², which reduces the risk of Hand-Arm Vibration Syndrome and improves operator endurance during prolonged finishing sessions.
Tool Longevity and Maintenance in Heavy Industry
Continuous industrial use demands strict adherence to duty cycles. High-speed motors generate thermal stress during 30-minute intervals of constant operation. Effective cooling paths are essential to prevent coil failure. Protection against metallic shavings is achieved through sealed bearing assemblies and non-conductive housings. Standardizing on a 3.2mm shank diameter, the common interface for the dremel, allows global procurement teams to streamline accessory inventory. This standardization can reduce localized supply chain costs by 15% across multi-national industrial sites. Rigorous adherence to these specifications ensures that precision tools meet the reliability standards expected in high-stakes environments like cryogenic service or high-pressure steam systems.
Operational Standards: Maintaining Material Integrity and Safety
Operational precision during valve seat lapping or component deburring hinges on the mitigation of metallurgical degradation. When utilizing a dremel rotary tool for high-tolerance adjustments, technicians must prioritize thermal control. Excessive frictional heat can induce localized annealing, which reduces the surface hardness of 410 stainless steel components below the required 30-35 HRC specification. This compromise in material integrity leads to premature erosion in high-velocity flow conditions. Maintaining a consistent RPM and applying intermittent pressure prevents the formation of heat-affected zones that could otherwise lead to stress corrosion cracking in high-pressure service.
Preventing Material Contamination
Cross-contamination represents a primary failure mode in corrosive environments. Using a carbon steel abrasive bit on a Monel 400 or Inconel 625 valve body introduces free iron particles into the alloy surface. This creates galvanic cells that initiate localized pitting. Maintenance facilities should maintain segregated tool sets, clearly labeled for specific material grades to avoid this risk. For components in oxygen or hydrogen service, all rotary attachments must undergo ultrasonic cleaning to meet CGA G-4.1 standards. This ensures zero hydrocarbon residue remains on the refined surfaces, preventing catastrophic ignition risks.
Safety and Compliance in Maintenance
Safety in petrochemical environments necessitates strict adherence to ATEX Directive 2014/34/EU. High-speed grinding with a dremel generates sparks that often exceed the ignition energy thresholds of Class I, Division 1 areas. Fire watch protocols must remain active for 60 minutes following any deburring activity. Technicians are required to wear impact-resistant eye protection and respiratory gear capable of filtering 0.3-micron metallic dust. Every maintenance action must be documented in the asset’s digital logbook to ensure traceability according to API 6D standards.
Post-maintenance quality control is the final barrier to operational failure. Technicians must perform a 100% visual inspection of all refined surfaces using 10x magnification. If the specification requires it, liquid penetrant testing confirms the absence of surface-breaking defects that aren’t visible to the naked eye. Verifying the surface finish (Ra) with a profilometer ensures the component meets the original equipment manufacturer’s sealing requirements. It’s vital that these steps are never bypassed during field repairs.
For technical support on maintaining high-performance hardware and ensuring long-term asset reliability, consult the engineering experts at OG VALVES LTD.
Strategic Integration: Enhancing Valve Reliability Through Precision
The integration of high-speed rotary tools, such as the dremel, into industrial maintenance cycles is a technical necessity for maintaining system integrity. High-pressure environments demand exact tolerances that manual filing or abrasive paper cannot achieve. Technicians must be trained to use these precision tools for tasks like removing localized corrosion or smoothing internal casting irregularities in critical infrastructure. A surface finish improved from Ra 3.2 to Ra 0.8 microns often results in a measurable extension of seal life by reducing friction-induced wear. This technical focus ensures that industrial valve performance meets API 6D and ASME B16.34 standards over extended service intervals.
Precision work on critical assets requires a clinical approach to tool application. Using a dremel allows for targeted material removal without compromising the structural thickness of the valve body. This level of control is vital when working with specialized alloys like Monel or Hastelloy. Engineers prioritize this surgical precision to prevent the propagation of stress fractures that often originate from microscopic surface defects. Reliable infrastructure depends on these minute details.
Developing a Precision Maintenance Culture
Transitioning from reactive repair to proactive refinement requires standardized operating procedures. When servicing ball valves, technicians utilize precision tools to restore seat contact surfaces to specific tolerances. This meticulous approach reduces fugitive emissions by up to 15 percent according to ISO 15848-1 leak rate data. The ROI is quantified through decreased downtime and a 12 percent reduction in emergency replacement costs. Maintenance teams that adopt these standards see fewer catastrophic failures in high-cycle applications.
Procurement and Support from OG Valves
OG Valves provides high-specification components engineered for long-term maintainability in oil, gas, and water treatment sectors. Our technical support teams assist engineers in selecting material grades, such as duplex stainless steel or forged carbon steel, that respond well to precision maintenance protocols. Global logistics networks ensure that critical components reach sites within 48 to 72 hours, minimizing operational interruptions. By leveraging our technical expertise, procurement specialists secure assets that offer superior lifecycle management and adherence to rigorous safety standards. We provide the technical data required to maintain peak performance across the entire lifespan of the component.
Optimizing Industrial Infrastructure Through Precision Engineering Standards
Effective valve maintenance in 2026 requires a transition from traditional grinding to high-precision surface refinement. Integrating a specialized dremel tool into your maintenance workflow allows for the removal of microscopic burrs without compromising the base material’s dimensional stability. This technical approach ensures that critical components meet the strict 0.4 micrometer Ra surface finish requirements found in 600 PSI steam systems. Adhering to these specifications significantly reduces the risk of premature seal failure and fugitive emissions across your pipeline assets.
Maintaining system integrity depends on sourcing components that exceed standard performance metrics. OG Valves provides engineering solutions that strictly follow ISO 9001 and API standard compliance protocols. Our team offers deep technical expertise in material grades like Inconel 625 and Monel 400 for aggressive corrosive service. We recognize that downtime isn’t an option for critical infrastructure; that’s why we offer global fast-track delivery to keep your operations running. It’s essential to align your maintenance strategies with these rigorous quality benchmarks to ensure long-term reliability. Consult with OG Valves for High-Specification Industrial Components today. Your facility’s safety and performance are within reach through these advanced engineering practices.
Frequently Asked Questions
Can a standard rotary tool be used on industrial stainless steel valves?
Standard rotary tools function on industrial stainless steel valves for light surface remediation but lack the torque for heavy material removal. Grade 316L stainless steel has a Brinell hardness of approximately 175 HB. This requires high-performance bits to prevent tool stall. Engineers should prioritize corded models that maintain constant speed under load to ensure consistent metal removal rates during maintenance cycles.
What is the best accessory for deburring a valve seat?
Tungsten carbide burrs with a double-cut pattern are the optimal accessories for deburring valve seats. These bits effectively remove burrs from cast steel or forged components without clogging. A 3mm or 1/8-inch shank size fits most industrial collets. Using a 60-grit aluminum oxide stone provides a secondary finishing stage to ensure the seat meets ISO 5208 leakage rate requirements during pressure testing.
How do I avoid over-grinding when using a rotary tool on critical components?
Maintaining precise control with a dremel or similar rotary tool requires using a dedicated plunge base or depth stop attachment. Critical valve components often have tolerances within 0.025 millimeters. Operators must utilize the lowest effective RPM to prevent heat-induced warping. Checking progress every 30 seconds with a digital micrometer ensures the component stays within the engineering specifications defined by ASME B16.34 standards.
Are there cordless rotary tools suitable for offshore oil and gas environments?
Cordless rotary tools are suitable for offshore environments if they possess an IP54 rating for dust and moisture resistance. High-capacity 12V lithium-ion batteries provide the necessary runtime for remote platform maintenance. These tools eliminate trip hazards from power cords on grated walkways. Technicians must ensure battery housings are sealed to prevent salt spray corrosion, which can degrade electrical contacts within 90 days of exposure.
What RPM is recommended for polishing valve stems?
A rotational speed between 12,000 and 15,000 RPM is recommended for polishing valve stems to a mirror finish. Using a felt polishing wheel with a diamond-based compound achieves the necessary smoothness. High speeds reduce the risk of creating flat spots on the cylindrical surface. This process targets a surface roughness of 0.2 to 0.4 Ra, which is essential for maintaining the integrity of the packing gland seal.
How does surface finish (Ra) affect the sealing performance of a globe valve?
Surface finish directly impacts the fugitive emission levels and sealing efficiency of globe valves. A finish of 1.6 Ra or better is typically required for metal-to-metal seating surfaces to prevent bypass leakage. If the Ra value exceeds 3.2, the risk of seal degradation increases by 25 percent over 1,000 cycles. Precise finishing ensures that the valve meets API 622 standards for low-emission packing performance in high-pressure systems.
Can rotary tools be used in explosive or ATEX-rated zones?
Electric rotary tools are strictly prohibited in ATEX-rated Zone 0 or Zone 1 environments due to the risk of internal sparking. These tools don’t meet the requirements for intrinsic safety in explosive atmospheres. Maintenance teams must utilize pneumatic rotary tools that operate on compressed air to eliminate ignition sources. All equipment used in these zones must carry the CE EX mark and comply with Directive 2014/34/EU.
What is the difference between a rotary tool and a die grinder for valve work?
The primary difference lies in the collet size and motor power output. A standard dremel uses a 1/8-inch collet for high-precision finishing, while an industrial die grinder utilizes a 1/4-inch collet for aggressive material removal. Die grinders often feature 0.5 horsepower motors, which is significantly higher than the 0.1 horsepower found in precision tools. This distinction determines whether the tool is used for heavy casting cleanup or delicate seat lapping.
 Responsive Menu