Emergency Industrial Valve Supplier UK: Rapid Response for Critical Infrastructure
May 05, 2026
Home+Emergency Industrial Valve Supplier UK: Rapid Response for Critical Infrastructure
Unplanned downtime in critical infrastructure represents a significant threat to both fiscal stability and environmental safety. You recognize that the pressure to restore operations often conflicts with the necessity for absolute component integrity, particularly when dealing with corrosive or high-pressure media. Securing a reliable emergency industrial valve supplier uk is therefore a prerequisite for maintaining operational continuity during localized system breaches. This requirement demands a partner capable of providing immediate access to high-specification alloys without the standard 12-week manufacturing lead times.
This comprehensive guide provides a technical framework for identifying and partnering with a supplier that prioritizes industrial precision and safety. We’ll examine how to mitigate the severe economic impacts of downtime through rapid procurement while ensuring full compliance with the updated safety requirements of BS EN 16668:2025. You’ll learn the criteria for selecting a partner that provides full technical documentation and fast-track logistics to any global site. Our analysis follows a methodical progression from identifying a technical need to executing a compliant replacement under extreme time constraints.
Key Takeaways
Identify the critical role an emergency industrial valve supplier uk plays in reducing the financial impact of unplanned downtime within the petrochemical and power sectors.
Recognize the essential valve specifications, including gate and ball valves, required for immediate isolation and replacement in high-pressure infrastructure.
Establish rigorous quality benchmarks using API 600 and ASME B16.34 standards to ensure component safety is never compromised for procurement speed.
Optimize supply chain efficiency by leveraging UK-based distribution hubs and fast-track logistics to minimize transit times for critical industrial hardware.
Learn how partnering with a specialist like OG VALVES LTD. provides access to comprehensive technical documentation and a high-specification inventory for urgent repairs.
The Role of an Emergency Industrial Valve Supplier in Critical Infrastructure
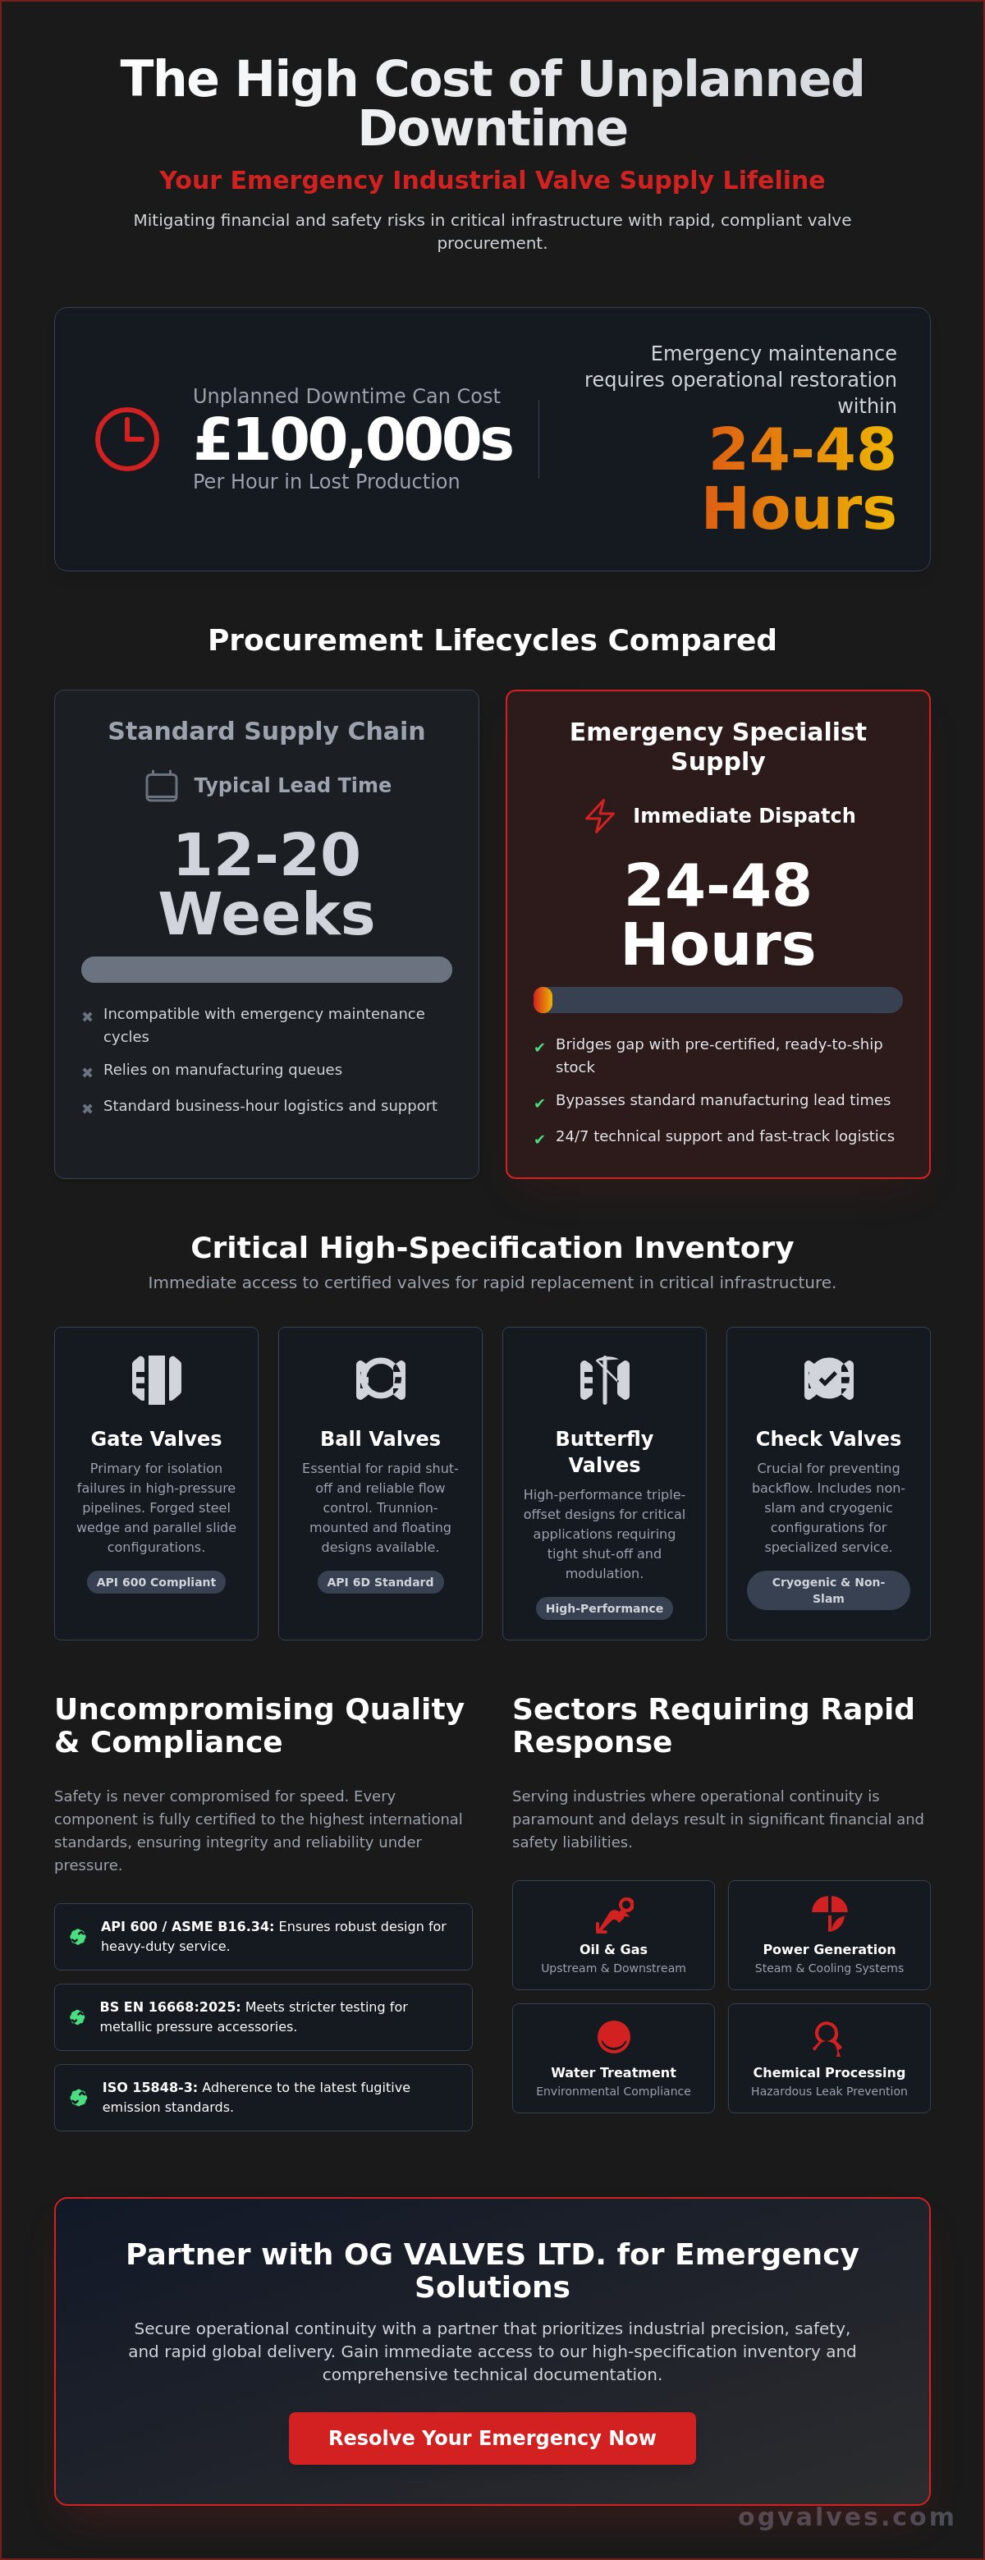
The role of an emergency industrial valve supplier uk is defined by the capacity to provide immediate, documented solutions for high-stakes mechanical failures. Unlike general distributors who prioritize volume and stock-turn over technical depth, an emergency specialist maintains a standing inventory of high-specification components such as Super Duplex gate valves or cryogenic check valves. The UK industrial valve market, projected to reach a value of £1.2 billion in 2026, operates on a foundation of continuous process integrity. When a critical component fails in a petrochemical refinery or power station, the economic impact is measured in hundreds of thousands of pounds per hour of lost production. Standard procurement lead times, which often extend to 12 or 20 weeks for specialized forged steel valves, are fundamentally incompatible with emergency maintenance cycles that require restoration within 24 to 48 hours. A specialist supplier bridges this gap by holding pre-certified stock that meets ASME and API specifications, ready for immediate dispatch to critical infrastructure sites.
Defining Emergency Valve Procurement
Emergency procurement represents a shift from scheduled maintenance planning to high-pressure reactive replacement. It necessitates 24/7 technical support and instantaneous inventory access to bypass typical quotation and manufacturing queues. While standard vendors operate on business-hour logistics, an emergency supplier functions as a strategic partner in risk mitigation, ensuring that every replacement valve meets the precise mechanical and chemical requirements of the existing system. This specialized service model prioritizes engineering compliance and speed of delivery over cost-minimization strategies common in non-critical procurement.
Sectors Requiring Rapid Response Supply
Upstream and downstream oil and gas facilities require immediate access to industrial valves that comply with API 6D and ISO 14313 standards to prevent catastrophic pressure loss. In the power generation sector, managing steam and cooling system failures requires valves capable of withstanding extreme thermal cycles. This is particularly relevant with the implementation of BS EN 16668:2025 on February 18, 2025, which introduces stricter testing for metallic valves used as pressure accessories. Water treatment and chemical processing plants also rely on rapid supply to prevent environmental non-compliance and hazardous leaks. These sectors demand components that adhere to the latest fugitive emission standards, such as the Class AQ requirements introduced in ISO 15848-3, which mandates a leakage rate of ≤0.1 ppm. For these operators, a delay in procurement isn’t just an operational inconvenience; it’s a significant threat to safety and regulatory standing.
Critical Valve Specifications for Rapid Replacement
Procuring a replacement component during a system failure requires immediate access to a physical inventory that mirrors the exact technical specifications of the damaged unit. A specialized emergency industrial valve supplier uk maintains stock based on the functional requirements of critical infrastructure, focusing on high-pressure and high-temperature performance. While standard lead times for bespoke valves can exceed several months, rapid response procurement relies on the availability of new, fully certified hardware. Managing Fast-Track Logistics effectively means overcoming the “just-in-time” supply chain vulnerabilities that often paralyze industrial operations during localized crises.
Gate valves remain the primary requirement for isolation failures in high-pressure pipelines. Inventory typically includes API 600 compliant forged steel wedge gates and parallel slide configurations designed for heavy-duty service. For applications requiring rapid shut-off and flow control reliability, trunnion-mounted or floating ball valves are essential. These components must adhere to API 6D standards to ensure bi-directional sealing integrity under fluctuating pressures. Butterfly valves, particularly triple-offset designs, and non-slam check valves provide critical protection against system surges and backflow, maintaining the mechanical stability of the broader network. You can review these technical parameters in our Industrial valves: The engineer’s comprehensive guide.
High-Specification Material Readiness
Emergency inventory must include advanced alloys to handle corrosive or cryogenic environments. This includes a standing stock of Super Duplex (ASTM A890), Stainless Steel (316/316L), and Forged Steel (A105) components. With the ISO 14313 revision introducing new requirements for hydrogen-embrittlement-resistant materials in 2025, ensuring material grades match existing system specifications exactly is a prerequisite for safety. Procurement specialists don’t just look for a valve; they require a specific metallurgical profile that guarantees long-term performance under stress. For immediate technical consultation on material compatibility, you should contact OG VALVES LTD. directly through our official site.
Size and Pressure Class Availability
Operational readiness demands a range of sizes and pressure ratings. A dependable supplier maintains inventory from 0.5-inch needle valves for instrumentation to large-bore butterfly valves for main headers. Compliance with ASME B16.34 is mandatory across all pressure classes, from Class 150 through to Class 2500. New standards such as ISO 5210:2026 and ISO 5211:2026, scheduled for release in February 2026, specify the interface requirements between actuators and valves. Having these compliant interfaces in stock ensures that replacement valves can be integrated into existing automated systems without the need for extensive field modifications.
Quality Assurance and Compliance Standards in Emergency Procurement
The primary risk in urgent procurement is the prioritisation of delivery speed over mechanical integrity. A professional emergency industrial valve supplier uk mitigates this risk by ensuring that every component in their inventory adheres to the UK Pressure Equipment (Safety) Regulations 2016. Speed must never serve as a justification for bypassing the rigorous design benchmarks established by API 600 or ASME B16.34. In high-pressure environments, such as those found in the UK’s petrochemical sectors, a non-compliant valve represents a significant point of failure that can lead to catastrophic system breaches. It’s essential that procurement teams verify that rapid-response hardware isn’t merely available but is technically equivalent to the original specification.
Positive Material Identification (PMI) is a critical protocol for verifying the metallurgical composition of valves before they leave the warehouse. This process prevents the accidental installation of incorrect alloys, which could lead to rapid corrosion or stress-induced fracturing. Every valve supplied under emergency conditions must be accompanied by full certification, specifically EN 10204 3.1 or 3.2. This documentation provides the necessary verification that the material properties and manufacturing processes meet the required technical specifications. Without this level of detail, the integrity of the entire pressure system is compromised.
Rigorous Testing Protocols for Emergency Stock
Before dispatch, every valve undergoes hydrostatic and pneumatic pressure testing to verify seat and shell integrity. For high-stakes applications, such as hydrogen or cryogenic service, additional Non-Destructive Testing (NDT) like dye penetrant or ultrasonic inspection is required. These protocols ensure that isolation valves meet zero-leakage standards, particularly under the duress of emergency operational restarts. The goal is to provide a component that is ready for immediate service without further field verification. A reliable emergency industrial valve supplier uk should provide these test results as part of the standard delivery package.
Documentation and Traceability
Immediate digital access to mill test reports (MTRs) and quality control records is a prerequisite for modern emergency supply. This transparency allows engineers to verify compliance before the physical component arrives on site. Maintaining a clear audit trail is essential for insurance purposes and regulatory compliance, particularly when replacing critical infrastructure components. For a deeper understanding of these requirements, refer to our A technical guide to industrial gate valves. This level of traceability ensures that long-term safety isn’t sacrificed for short-term operational continuity.
Managing Fast-Track Logistics and Global Lead Times from the UK
The United Kingdom functions as a primary strategic hub for the global distribution of high-specification flow control components. An emergency industrial valve supplier uk must leverage this geographical advantage to provide rapid response capabilities to both domestic and international critical infrastructure. Efficient logistics involve the coordination of heavy-lift transport and expedited customs clearance to ensure that critical components, such as trunnion-mounted ball valves or large-bore butterfly valves, reach their destination without administrative delay. With the UK industrial valve market expected to add more than $1.08 billion in value between 2026 and 2031, the infrastructure supporting these shipments is increasingly sophisticated and reliable.
Reducing transit times for heavy industrial hardware requires dedicated logistics partners who specialize in over-dimensional cargo. For international shipments, navigating the complexities of export documentation and compliance with local regulatory frameworks is essential to avoid port-side impoundment. Real-time tracking and comprehensive project management provide engineers with precise delivery windows, allowing for the accurate scheduling of maintenance crews and crane hire. It’s not just about moving a product; it’s about managing a timeline where every hour represents a quantifiable financial loss.
National vs. International Emergency Supply
Domestic facilities benefit from same-day dispatch protocols, often receiving replacements within hours via dedicated road freight. For offshore installations or global sites in the Middle East or North Sea, air freight strategies are employed. This includes the use of chartered cargo flights to transport mission-critical hardware like Understanding industrial check valves to remote locations. These logistics networks are designed to operate 24/7, ensuring that geographical distance doesn’t dictate the duration of unplanned downtime. When a system is compromised, the speed of the supply chain is as vital as the quality of the component.
Reducing Lead Times through Strategic Stocking
Strategic inventory management allows for the immediate availability of shelf-ready valves that meet the latest standards, such as ISO 5211:2026, which specifies the interface between actuators and valves. By collaborating directly with manufacturers to maintain a rolling stock of high-spec forged steel and alloy components, a supplier can bypass standard 12-week production queues. This proactive approach significantly reduces the total cost of ownership by preventing the exponential losses associated with extended facility outages. If your facility requires immediate component replacement to restore operational integrity, view our current high-specification inventory to secure a rapid solution.
Partnering with OG VALVES LTD. for Emergency Industrial Solutions
OG VALVES LTD. operates as a specialized emergency industrial valve supplier uk, providing the technical infrastructure required for the immediate replacement of mission-critical components. Our operational model is built on the immediate availability of high-specification hardware, including gate, ball, globe, check, and butterfly valves. We recognize that in sectors such as oil, gas, and power generation, the cost of mechanical failure is absolute. Therefore, our inventory is maintained to meet the most rigorous international standards, ensuring that every replacement component provides equivalent or superior performance to the unit it replaces. Our UK-based distribution center is optimized for fast-track delivery to any global industrial site, managing the complexities of logistics and documentation to facilitate rapid site restoration.
Why Industrial Leaders Trust OG VALVES
Industrial leaders prioritize OG VALVES because of our clinical focus on engineering excellence and long-term durability. We provide direct access to technical specialists who understand the complexities of ASME B16.34 and API 600. With the UK industrial valve market projected to grow at a compound annual growth rate of 7.75% from 2025 to 2032, the demand for high-integrity components has never been higher. Our commitment to quality is validated through comprehensive testing protocols, including hydrostatic and pneumatic verification. We serve as a dependable partner that understands the functional reality of heavy industry, prioritizing safety and compliance over marketing hyperbole.
Standing inventory of Super Duplex, Stainless Steel, and Forged Steel components.
Strict adherence to API, ASME, and ISO international standards.
Comprehensive technical documentation (EN 10204 3.1/3.2) provided with every dispatch.
Expert support for identifying material compatibility in corrosive or high-pressure environments.
Initiating an Emergency Procurement Request
To facilitate rapid procurement, our quoting process is streamlined for an immediate response. Engineers and procurement specialists must provide specific technical data to ensure accurate valve identification and system compatibility. This includes the required valve type, bore size, pressure class (e.g., ASME Class 1500), and material grade. Providing the relevant design standard and any specific fugitive emission requirements, such as the ISO 15848-3 Class AQ standard, allows our team to verify stock compatibility instantly. This methodical approach ensures that the replacement valve meets all regulatory and operational requirements without delay. For immediate assistance with critical infrastructure failures, you should Contact OG VALVES LTD. for emergency industrial valve supply.
Securing System Integrity through Strategic Procurement
Maintaining operational continuity in the petrochemical and power sectors requires a shift from standard vendor relationships toward a technical partnership. Selecting a reliable emergency industrial valve supplier uk ensures that unplanned downtime is mitigated through immediate access to high-specification hardware that adheres to the latest standards, including BS EN 16668:2025. System integrity depends on the absolute verification of material grades and pressure classes under extreme time constraints. It’s essential that speed never compromises the engineering benchmarks required for safe operation.
OG VALVES LTD. provides the necessary engineering precision to manage these high-stakes scenarios. Our extensive stock of API and ASME certified valves, combined with global fast-track delivery capabilities, allows for the rapid restoration of critical infrastructure. We provide specialist expertise in high-pressure and corrosive service, ensuring that every replacement component meets the rigorous demands of your existing network. By prioritizing technical compliance and documentation, you protect your facility from the long-term risks of substandard components. Request an Emergency Quote from OG VALVES LTD. to ensure your critical infrastructure remains protected by high-specification engineering.
Frequently Asked Questions
What defines an emergency industrial valve supplier?
An emergency supplier maintains a standing inventory of high-specification components for immediate dispatch to critical infrastructure sites. Unlike general distributors, an emergency industrial valve supplier uk prioritizes technical compliance and risk mitigation over standard stock-turn models. This specialized service ensures that replacement valves meet exact engineering requirements to restore operations within hours rather than the 12 to 20 weeks typical of standard procurement.
Can high-spec valves like super duplex be supplied on an emergency basis?
Yes, high-specification valves in materials such as Super Duplex (ASTM A890) or Stainless Steel (316L) are available for immediate procurement. These alloys are essential for corrosive or high-pressure service in the petrochemical and offshore sectors. Maintaining these material grades in stock allows operators to bypass production queues, ensuring that material integrity isn’t sacrificed for delivery speed during a localized system failure.
How do you ensure quality compliance during a fast-track delivery?
Quality is maintained through rigorous adherence to API 600 and ASME B16.34 standards regardless of the delivery urgency. Every valve undergoes hydrostatic and pneumatic pressure testing before it leaves the facility to verify seat and shell integrity. Positive Material Identification (PMI) is also performed to verify the metallurgical composition, ensuring that the component matches the required chemical specification exactly.
What information is needed to request an emergency valve replacement?
Requesting a rapid replacement requires precise technical data to ensure absolute system compatibility. You must provide the valve type, bore size, pressure class (e.g., ASME Class 1500), and material grade. Including the design standard, such as API 6D or ISO 14313, and any specific requirements for fugitive emissions helps an emergency industrial valve supplier uk identify the correct component and provide a technical quote instantly.
Do you supply valves for offshore oil and gas facilities?
We provide high-specification valves specifically designed for the demanding requirements of offshore oil and gas facilities. This includes trunnion-mounted ball valves and non-slam check valves that comply with API 6A and 6D standards. Logistics for remote offshore sites are managed via specialized air freight to minimize transit times and restore production integrity as quickly as possible under extreme operational conditions.
What are the typical lead times for emergency valve shipping from the UK?
Typical lead times for domestic UK deliveries involve same-day dispatch, with components often reaching sites within 4 to 8 hours via dedicated road freight. International shipments to global industrial hubs generally arrive within 24 to 48 hours when using expedited air freight services. These timelines are managed through established logistics networks that specialize in heavy-lift and over-dimensional industrial cargo to avoid port-side delays.
Are your emergency valves supplied with full technical documentation?
Every component is supplied with a comprehensive technical documentation package as a standard requirement. This includes EN 10204 3.1 or 3.2 certification, mill test reports (MTRs), and pressure test results. Providing this documentation digitally before the hardware arrives allows engineers to verify compliance and maintain a clear audit trail for regulatory and insurance purposes, ensuring long-term safety and traceability.
Can you provide actuated valves on an emergency basis?
Actuated valves can be supplied on an emergency basis by utilizing standardized interface protocols for rapid assembly. We ensure that valves meet the latest ISO 5211:2026 requirements for multi-turn and part-turn actuator attachments. This allows for the immediate integration of replacement valves into existing automated systems, ensuring that both mechanical flow control and electronic monitoring are restored without the need for extensive field modifications.
 Responsive Menu